
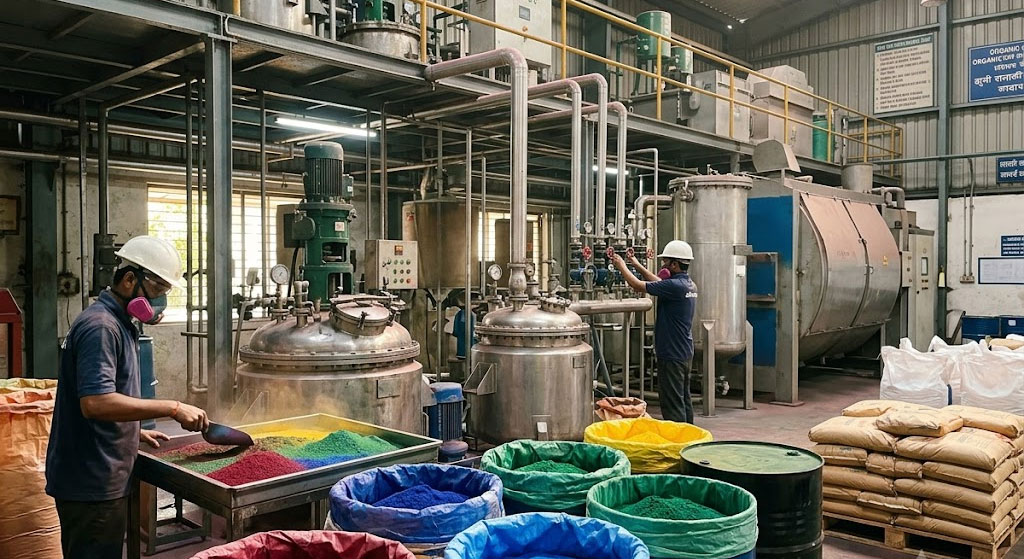
High-Performance Organic Pigments for Printing Ink, Plastic, Paint & Coating Industries
The global demand for high-performance organic pigments has increased rapidly due to expanding industrial manufacturing sectors such as printing inks, plastics, paints, coatings, packaging, textiles, automotive, and specialty chemicals. Industries worldwide require pigments that provide excellent color strength, heat stability, dispersion properties, chemical resistance, and long-term durability for modern manufacturing applications.
India has become one of the leading global manufacturing hubs for organic pigments because of its advanced chemical production capabilities, export infrastructure, competitive manufacturing advantages, and ability to serve large-scale industrial buyers worldwide.
Megha International supplies industrial-grade organic pigments designed for demanding applications across multiple industries where consistent color quality, process stability, and export-grade performance are essential.
Organic pigments are widely used by:
- printing ink manufacturers
- plastic masterbatch companies
- paint manufacturers
- coating industries
- flexible packaging converters
- textile printing industries
- PVC product manufacturers
- rubber processing industries
As industries increasingly focus on vibrant colors, environmental compliance, product consistency, and advanced material performance, the demand for high-quality organic pigments manufacturers in India continues to grow across international markets.
What Are Organic Pigments?
Organic pigments are carbon-based colored compounds used to impart color to industrial products and materials. Unlike dyes, pigments are insoluble substances that remain dispersed within the application medium rather than dissolving completely.
Organic pigments are known for:
- bright shades
- high tinting strength
- excellent transparency
- superior color brilliance
- good dispersion
- wide shade availability
They are extensively used in:
- printing inks
- paints
- plastics
- coatings
- packaging materials
- synthetic fibers
- rubber products
- textile printing
How Organic Pigments Work
Pigments function by selectively absorbing and reflecting specific wavelengths of light, producing visible color.
The performance of industrial pigments depends on:
- particle size
- dispersion quality
- chemical structure
- heat resistance
- weather stability
- solvent resistance
Why Global Industries Prefer Organic Pigments
Organic pigments offer several advantages over traditional coloring systems.
High Color Strength
Organic pigments provide:
- vibrant shades
- rich coloration
- excellent tinting performance
This is important for:
- packaging graphics
- branding applications
- decorative coatings
- printing inks
Wide Shade Range
Industries require pigments in multiple colors for:
- product customization
- packaging design
- industrial branding
- aesthetic applications
Common shades include:
- reds
- yellows
- oranges
- blues
- greens
- violets
Excellent Dispersion Properties
Good dispersion improves:
- manufacturing consistency
- surface appearance
- print quality
- coating smoothness
This is critical in:
- ink manufacturing
- masterbatch production
- paint processing
Environmental Advantages
Modern organic pigments are increasingly designed for:
- low toxicity
- eco-friendly processing
- regulatory compliance
- sustainable industrial production
Global buyers often search for:
- heavy metal free pigments
- REACH compliant pigments
- RoHS compliant pigments
Types of Organic Pigments Used in Industries
Pigment Red Series
Widely used in:
- printing inks
- coatings
- plastics
- packaging applications
Features:
- strong brightness
- excellent tinting strength
- attractive visual appeal
Pigment Yellow Series
Used extensively for:
- plastic coloring
- paints
- flexible packaging
- industrial coatings
Advantages:
- heat stability
- strong opacity
- vibrant coloration
Pigment Blue Series
Commonly used in:
- ink industries
- plastic masterbatch
- decorative coatings
Key properties:
- chemical resistance
- excellent dispersion
- durability
Pigment Green Series
Used in:
- packaging printing
- industrial paints
- plastic compounds
Industries prefer these pigments for:
- color stability
- weather resistance
- industrial consistency
Applications of Organic Pigments
Printing Ink Industry
Organic pigments are heavily used in:
- gravure inks
- flexographic inks
- offset inks
- screen printing inks
- packaging inks
Industries require pigments with:
- high gloss
- strong color development
- print consistency
Plastic Masterbatch Industry
Plastic manufacturers use pigments in:
- PVC products
- household plastics
- automotive components
- packaging materials
- consumer products
Important properties include:
- heat resistance
- migration resistance
- dispersion quality
Paint & Coating Industry
Industrial coatings require pigments that provide:
- UV resistance
- weather durability
- color retention
- surface uniformity
Applications include:
- decorative paints
- industrial coatings
- automotive coatings
- protective coatings
Flexible Packaging Industry
Packaging industries use pigments for:
- branding
- product identification
- visual appeal
- packaging differentiation
This sector demands:
- excellent printability
- color consistency
- food packaging compatibility
Important Properties Buyers Look for in Organic Pigments
Heat Stability
Plastic and coating industries require pigments that withstand high processing temperatures.
Applications include:
- injection molding
- extrusion
- industrial coating curing
Light Fastness
Pigments used outdoors require resistance against:
- sunlight exposure
- fading
- weathering
This is critical for:
- automotive coatings
- outdoor plastics
- industrial paints
Chemical Resistance
Industrial applications require pigments resistant to:
- solvents
- chemicals
- oils
- industrial environments
Dispersion Quality
Better dispersion leads to:
- smooth manufacturing
- uniform coloration
- reduced production defects
Global Demand for Organic Pigments
The international market for organic pigments continues growing due to expansion in:
- packaging industries
- plastic manufacturing
- automotive production
- infrastructure development
- industrial coatings
- textile printing
Major importing regions include:
- UAE
- Saudi Arabia
- Turkey
- Bangladesh
- Vietnam
- Europe
- South Africa
- Latin America
Organic Pigments for Printing Ink Industry
The printing ink sector is one of the largest consumers of organic pigments.
Applications include:
- flexible packaging
- labels
- publication printing
- corrugated packaging
- industrial printing
Industries prefer pigments that provide:
- bright shades
- print clarity
- strong color strength
- fast processing performance
Organic Pigments for Plastic Industry
Plastic masterbatch industries require pigments with:
- thermal stability
- consistent dispersion
- low migration
- high opacity
Applications include:
- PVC pipes
- plastic containers
- woven sacks
- packaging films
- automotive plastics
Why International Buyers Source Organic Pigments from India
India is preferred globally because manufacturers can provide:
- competitive pricing
- export-scale supply
- multiple pigment grades
- technical support
- customized shades
- reliable export logistics
International buyers also value:
- manufacturing scalability
- consistent quality
- faster sourcing support
- industrial application expertise
Why Industries Choose Megha International
Megha International serves industrial buyers requiring reliable organic pigment solutions for demanding manufacturing applications.
The company focuses on:
- industrial-grade pigment quality
- export-oriented supply capability
- application-focused pigment solutions
- consistency in production
- support for multiple industries
Industries served include:
- printing inks
- plastics
- paints
- coatings
- packaging
- industrial manufacturing
Future of Organic Pigments Industry
Demand for organic pigments is expected to rise significantly because of:
- growing packaging industries
- increasing plastic consumption
- expanding infrastructure
- automotive production growth
- demand for sustainable color solutions
Future industrial trends include:
- eco-friendly pigments
- high-performance pigment technologies
- low-VOC systems
- advanced color formulations
- sustainable manufacturing
Conclusion
Organic pigments play a critical role across modern industrial manufacturing sectors by delivering vibrant shades, process stability, durability, and application performance. Industries worldwide increasingly require reliable pigment manufacturers capable of supplying export-quality products for printing inks, plastics, paints, coatings, and packaging applications.
Megha International supports global industries with industrial-grade organic pigment solutions designed for high-performance manufacturing applications and export-oriented industrial requirements.
As international demand for industrial pigments continues growing, manufacturers capable of maintaining consistent quality, technical expertise, and scalable export supply will remain key partners for global industrial buyers.
FAQs
What are organic pigments used for?
Organic pigments are used in printing inks, plastics, paints, coatings, packaging, textile printing, and industrial manufacturing applications.
What is the difference between dyes and pigments?
Dyes dissolve in the application medium, while pigments remain insoluble and dispersed within the material.
Which industries use organic pigments?
Printing ink, plastic masterbatch, paint, coating, packaging, rubber, and textile industries widely use organic pigments.
Why are organic pigments preferred in printing inks?
They provide vibrant colors, excellent dispersion, high tinting strength, and strong print quality.
Are organic pigments suitable for plastics?
Yes. Organic pigments are widely used for coloring PVC, packaging films, molded plastics, and industrial plastic products.
What properties are important in industrial pigments?
Heat stability, light fastness, chemical resistance, and dispersion quality are key industrial requirements.
Which countries import organic pigments from India?
UAE, Saudi Arabia, Turkey, Bangladesh, Vietnam, South Africa, and European countries are major importers.
What are heat resistant pigments?
Heat resistant pigments maintain color stability during high-temperature industrial processing applications.
Are organic pigments environmentally friendly?
Modern organic pigments are increasingly developed to support eco-friendly and regulatory-compliant industrial applications.
Why do international buyers source pigments from India?
India offers competitive pricing, export-scale production, technical expertise, and reliable industrial supply capabilities.