
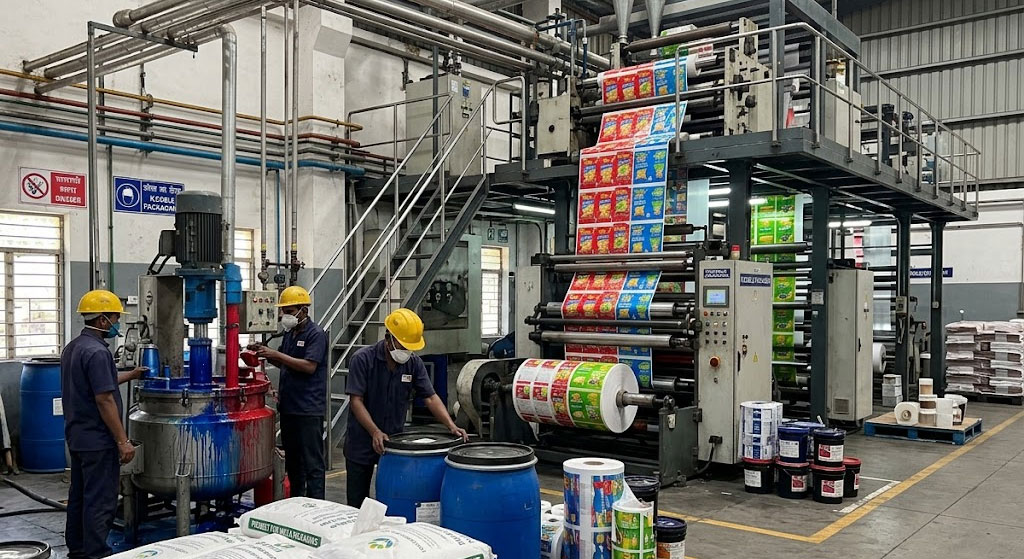
High-Performance Industrial Pigments for Gravure & Flexographic Packaging Applications
The global flexible packaging industry has experienced massive growth due to increasing demand from FMCG, food processing, pharmaceuticals, personal care, e-commerce, industrial packaging, and retail sectors. Flexible packaging manufacturers worldwide require high-performance pigments capable of delivering vibrant print quality, excellent color consistency, strong adhesion, and durable packaging appearance across modern printing systems.
As packaging industries continue expanding globally, the demand for industrial pigments for flexible packaging printing has increased significantly across international manufacturing markets.
Megha International supplies industrial pigment solutions designed for flexible packaging printing applications where print clarity, color consistency, industrial processing stability, and export-quality performance are critical for large-scale packaging production.
Packaging converters and printing ink manufacturers require pigments that provide:
- high color strength
- excellent dispersion
- print durability
- heat stability
- migration resistance
- gloss development
- chemical resistance
- consistent packaging appearance
Industries increasingly require reliable pigment manufacturers capable of supporting:
- gravure printing
- flexographic printing
- packaging inks
- industrial packaging production
- export-quality packaging standards
Why Pigments Are Important in Flexible Packaging Printing
Pigments are the primary coloring agents responsible for:
- packaging appearance
- brand identity
- print clarity
- product visibility
- shelf impact
In modern packaging industries, high-quality printing directly influences:
- consumer attraction
- product branding
- packaging differentiation
- market competitiveness
\text{Packaging Visual Impact} = \text{Pigment Quality} + \text{Print Clarity} + \text{Color Consistency}
Poor pigment quality may lead to:
- inconsistent shades
- weak print appearance
- poor gloss
- fading
- packaging rejection
Therefore packaging manufacturers require pigments capable of maintaining stable industrial printing performance.
Major Printing Processes Used in Flexible Packaging
Gravure Printing
Gravure printing is widely used for:
- food packaging
- FMCG packaging
- laminated films
- industrial packaging
Pigments used in gravure inks require:
- fine particle size
- excellent dispersion
- strong transparency
- smooth print transfer
Flexographic Printing
Flexographic printing is commonly used for:
- corrugated packaging
- labels
- flexible films
- retail packaging
Industries require pigments with:
- quick drying compatibility
- stable viscosity
- excellent print transfer
Types of Pigments Used in Flexible Packaging Printing
Organic Pigments
Organic pigments are preferred because they provide:
- vibrant shades
- high tinting strength
- excellent transparency
- attractive print quality
Applications:
- packaging inks
- labels
- decorative packaging
High Performance Pigments
Used in premium packaging applications requiring:
- chemical resistance
- heat stability
- migration resistance
- long-term durability
Applications include:
- food packaging
- pharmaceutical packaging
- specialty packaging
Specialty Packaging Pigments
Designed for:
- metallic effects
- premium branding
- luxury packaging
- visual enhancement
Major Industries Using Flexible Packaging Pigments
Food Packaging Industry
Food packaging manufacturers require:
- vibrant branding colors
- migration resistance
- safe packaging performance
Applications:
- snack packaging
- beverage packaging
- frozen food packaging
- processed food packaging
FMCG Packaging Industry
FMCG products rely heavily on:
- shelf appeal
- attractive printing
- strong branding visibility
Packaging applications include:
- detergent packaging
- cosmetic packaging
- personal care packaging
- household products
Pharmaceutical Packaging
Pharma packaging industries require:
- print clarity
- regulatory compliance
- durable packaging graphics
Applications:
- blister packaging
- medicine labels
- pharmaceutical pouches
Industrial Packaging
Industrial products use flexible packaging for:
- chemicals
- fertilizers
- industrial powders
- bulk materials
Industries require:
- strong print durability
- weather resistance
- industrial handling compatibility
Important Pigment Properties for Flexible Packaging Printing
Dispersion Quality
Excellent dispersion improves:
- print smoothness
- image sharpness
- color uniformity
- production consistency
Poor dispersion may cause:
- print defects
- uneven coloration
- production downtime
Color Strength
High color strength allows:
- lower pigment loading
- better print intensity
- efficient ink formulation
Heat Stability
Packaging printing involves:
- drying systems
- lamination processes
- industrial processing temperatures
Pigments must maintain:
- color stability
- print integrity
Migration Resistance
Food and pharmaceutical packaging industries require pigments resistant to:
- chemical migration
- contamination risks
This is especially important in:
- food-contact packaging
- pharmaceutical applications
Chemical Resistance
Packaging inks may encounter:
- oils
- moisture
- chemicals
- transportation stress
Pigments must resist:
- fading
- bleeding
- degradation
Why Flexible Packaging Industry Is Growing Rapidly
Global packaging demand is increasing because of:
- e-commerce growth
- FMCG expansion
- food processing industries
- pharmaceutical production
- retail packaging demand
Major growing packaging markets include:
- UAE
- Saudi Arabia
- Bangladesh
- Vietnam
- Turkey
- Africa
- Latin America
This creates strong international demand for industrial pigment suppliers.
Pigments Used in Laminated Packaging Films
Flexible laminated packaging requires pigments capable of supporting:
- multilayer printing
- lamination compatibility
- high-speed processing
Applications:
- snack pouches
- stand-up pouches
- industrial films
- retort packaging
Sustainable Trends in Packaging Printing
Packaging industries increasingly focus on:
- eco-friendly inks
- sustainable packaging
- low migration pigments
- regulatory-compliant materials
Global brands increasingly require:
- REACH compliant pigments
- environmentally responsible printing systems
- safer packaging solutions
especially for export packaging applications.
Why International Packaging Industries Source Pigments from India
India has become a major sourcing destination because manufacturers offer:
- industrial expertise
- export-oriented production
- scalable supply capability
- customized pigment solutions
- competitive manufacturing advantages
Packaging industries prefer suppliers capable of supporting:
- consistent industrial quality
- large-scale packaging production
- technical application support
Why Industries Choose Megha International
Megha International supports packaging and printing industries with industrial-grade pigment solutions designed for modern flexible packaging printing applications.
The company focuses on:
- industrial pigment consistency
- export-oriented supply capability
- application-focused packaging solutions
- support for industrial printing industries
- quality-driven manufacturing support
Industries served include:
- flexible packaging
- printing inks
- labels
- FMCG packaging
- food packaging
- pharmaceutical packaging
Future of Flexible Packaging Pigments
Future demand is expected to rise significantly because of:
- growing packaging consumption
- premium branding requirements
- industrial packaging expansion
- sustainable packaging trends
Future industry developments include:
- low migration pigments
- eco-friendly packaging systems
- advanced printing technologies
- sustainable ink formulations
- high-performance packaging pigments
Conclusion
Pigments play a critical role in modern flexible packaging printing by delivering vibrant branding colors, print consistency, packaging durability, and strong visual appeal across industrial packaging applications. As global packaging industries continue expanding, manufacturers increasingly require reliable pigment suppliers capable of supporting export-oriented and high-performance packaging production requirements.
Megha International supplies industrial pigment solutions designed for flexible packaging printing applications across food packaging, FMCG packaging, pharmaceutical printing, industrial packaging, and modern packaging manufacturing industries.
As packaging technologies continue evolving globally, experienced industrial pigment manufacturers capable of maintaining quality consistency, technical expertise, and scalable export supply capability will remain critical partners for modern packaging industries worldwide.
FAQs
What are pigments used for in flexible packaging printing?
Pigments provide color, branding visibility, print clarity, and packaging appearance in flexible packaging applications.
Which printing processes use packaging pigments?
Gravure printing and flexographic printing are the main processes used in flexible packaging industries.
Why are organic pigments preferred in packaging printing?
Organic pigments provide vibrant shades, high color strength, excellent transparency, and strong print quality.
What properties are important in packaging pigments?
Dispersion quality, heat stability, migration resistance, chemical resistance, and color strength are important.
What are low migration pigments?
Low migration pigments reduce chemical transfer in food and pharmaceutical packaging applications.
Which industries use flexible packaging pigments?
Food packaging, FMCG, pharmaceuticals, industrial packaging, labels, and retail packaging industries use industrial pigments.
Why is print quality important in packaging?
Packaging appearance directly affects branding, product visibility, and consumer attraction.
Which countries import packaging pigments from India?
UAE, Saudi Arabia, Bangladesh, Vietnam, Turkey, African countries, and global packaging markets import industrial pigments.
Why are sustainable pigments important in packaging industry?
Global brands increasingly require eco-friendly and regulatory-compliant packaging materials.
Why do international packaging industries source pigments from India?
India offers industrial expertise, export-scale manufacturing, customized pigment solutions, and reliable supply capability.